A successful lab route is the start of CDMO scale-up
A laboratory route can demonstrate that a molecule is accessible. Commercial API manufacturing asks a broader question: can the route be repeated safely, consistently, economically, and with the level of quality control the programme requires? The difference between those two questions is where much of the value of capable CDMO process development lies.
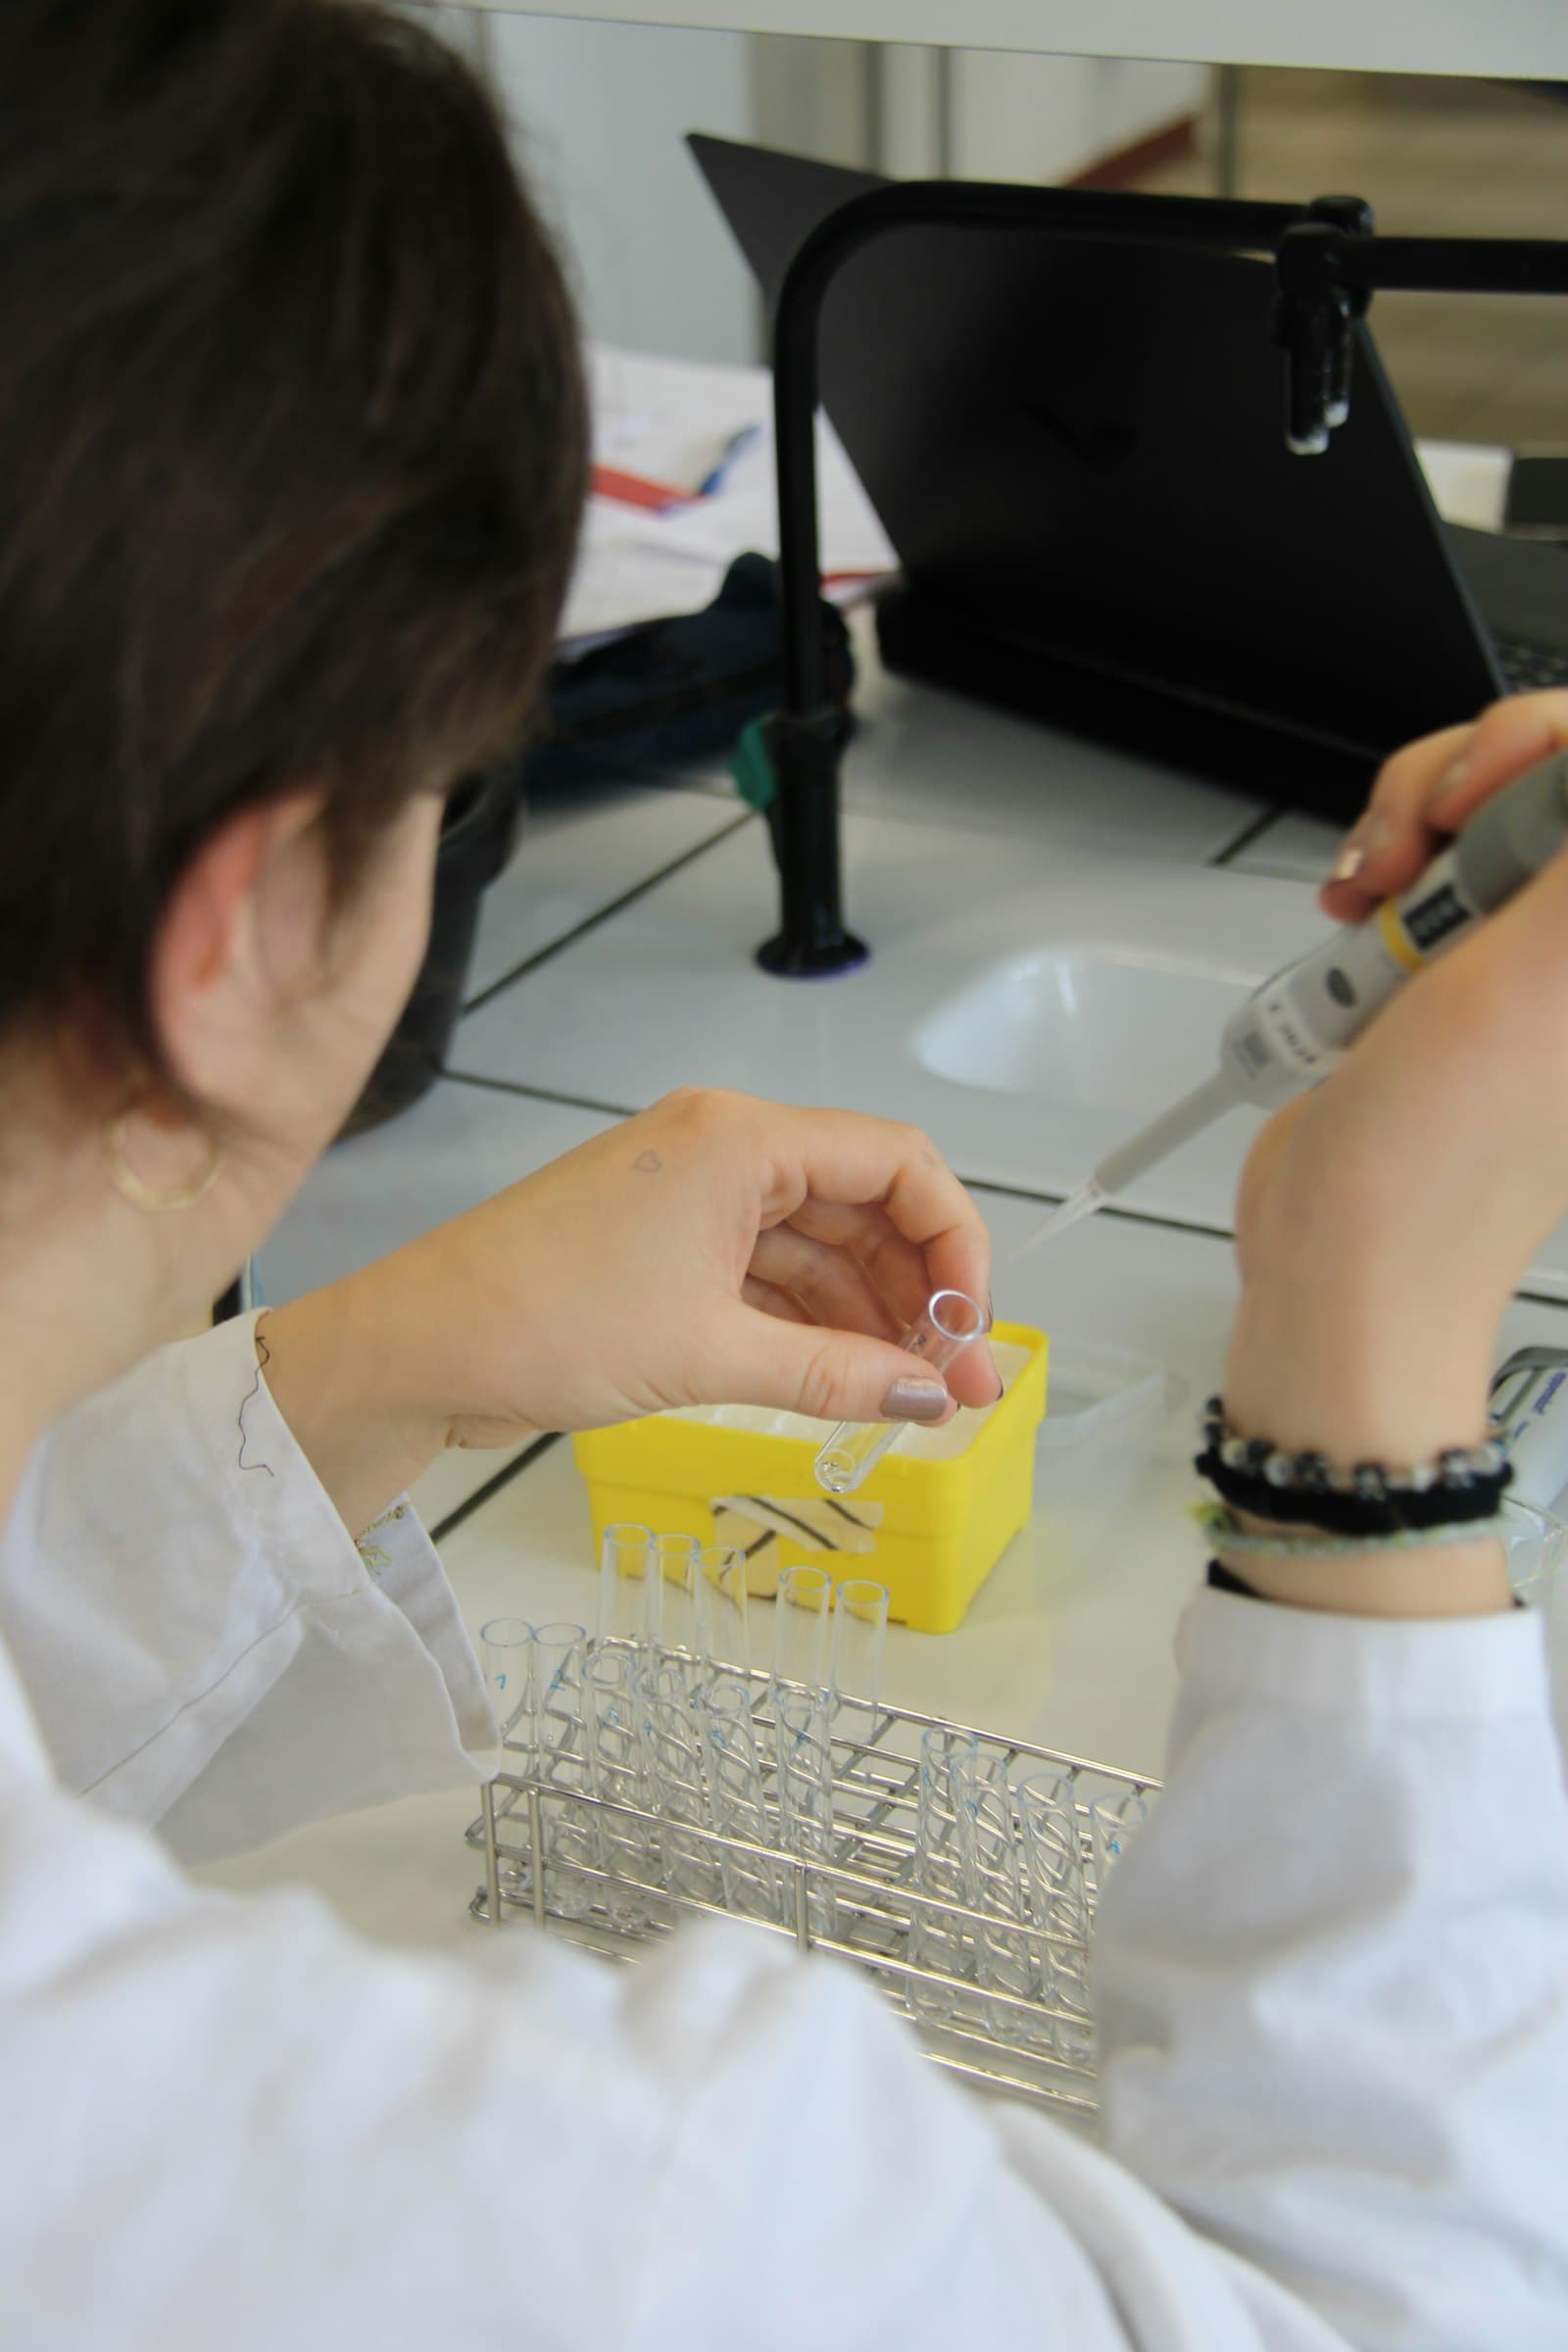
Scale-up is not simply a matter of increasing batch size. It requires teams to understand the critical reaction steps, impurity profile, raw-material availability, work-up behaviour, isolation method, analytical controls, and operational constraints that may become more important at plant scale. A well-prepared programme turns laboratory knowledge into a connected manufacturing plan rather than relying on a single successful experiment.
What a CDMO should review before technology transfer
Before a technology transfer begins, the development and manufacturing teams should align on what is known, what is assumed, and what still needs to be established. This normally includes the proposed manufacturing route, critical material attributes, reaction and isolation conditions, known impurities, analytical methods, specifications, available process safety information, and the intended timeline. A clear gap assessment prevents important questions from surfacing only after a campaign has been scheduled.
The review should also include the operational setting. Equipment fit, material handling, cleaning approach, sampling, filtration, drying, containment, and laboratory turnaround can all affect the commercial practicality of a route. A capable CDMO will translate these practical considerations into an experiment plan or transfer package that gives the customer team a realistic view of readiness.
Make process development trade-offs visible
Every route contains trade-offs. A change that improves yield may add cycle time; a readily available reagent may create a more demanding purification; a shorter route may increase sensitivity at one key step. Process development should make these choices visible so the programme can decide what matters most for its phase, market, and risk appetite.
The most useful development work focuses on uncertainty reduction. Depending on the molecule, this may involve understanding impurity purge, improving crystallisation behaviour, reviewing mixing and heat-transfer implications, testing raw-material variability, or strengthening the isolation approach. The goal is not to generate data for its own sake. It is to develop evidence that supports a robust manufacturing decision and an easier transition to commercial API production.
Plan analytical, quality, and plant readiness together
Technology transfer is strongest when development, analytical, quality, engineering, production, and supply functions are involved before the first manufacturing campaign. Analytical methods need to be ready for the planned sampling points and release timeline. Batch-record expectations need to reflect the operating sequence. Material specifications, quality agreements, and documentation responsibilities should be established well before a delivery date is at risk.
This cross-functional preparation reduces the gap between a process that works in theory and a process that can be run reliably in a commercial plant. It also gives the programme a clear way to manage open items. Rather than treating gaps as failure, teams can prioritise them, assign ownership, and define how learning from the first campaign will be incorporated into the next one.
Measure CDMO capability by the quality of the conversation
When selecting a CDMO for API scale-up, equipment and capacity are essential, but they are not the whole decision. The quality of the technical conversation is often revealing. Does the team ask precise questions about route history, control strategy, material sources, impurity risks, and timelines? Can it explain how findings will be documented, reviewed, and transferred to the plant? Does it identify trade-offs clearly rather than offering a generic assurance?
A capable development partner creates transparency around the work required to reach commercial readiness. That helps sourcing and development teams budget accurately, sequence work sensibly, and make decisions with a clearer understanding of risk. It also establishes the collaborative working style that will matter when the programme moves from development batches to routine manufacture.
From first batch to a commercial manufacturing platform
The first scale-up batch should be managed as a controlled learning opportunity. Teams should agree in advance what data will be reviewed, which observations would trigger further development, and how the outcome will inform the next campaign. That discipline makes it possible to improve the process without losing sight of quality, schedule, and product intent.
Ultimately, commercial success comes from a connected approach: a practical route, evidence-based process development, plant-ready documentation, reliable analytical support, and clear governance between the sponsor and CDMO. When these elements are aligned, technology transfer becomes a managed progression toward dependable API supply rather than a handoff filled with avoidable surprises.
Have a programme or sourcing decision to discuss?
Partner with NASPL