Core Capabilities

Two complementary cGMP units connecting intermediates, specialist chemistry, and commercial API manufacturing.

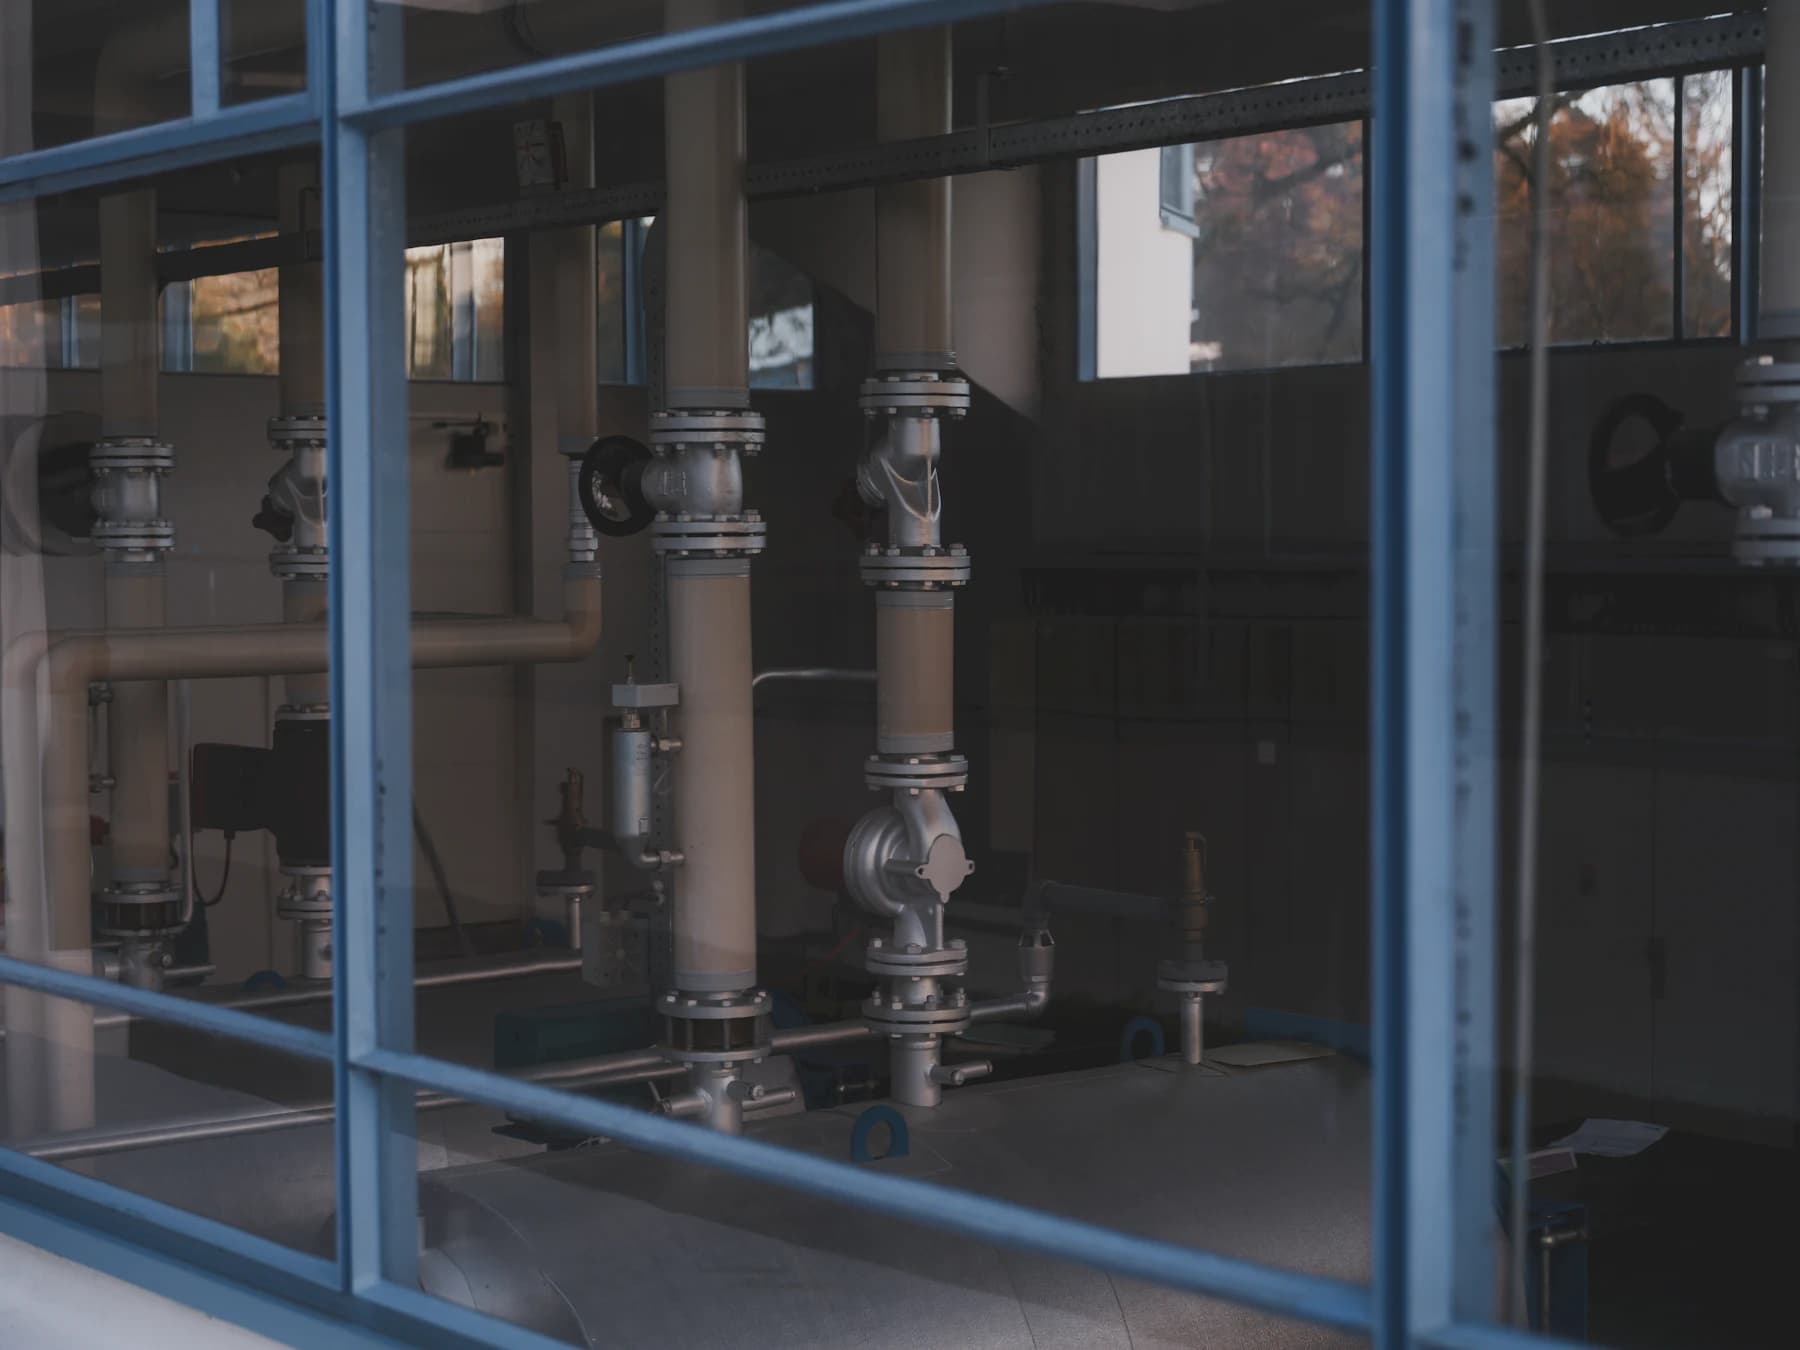
Industrial process piping inside a manufacturing facility

Intermediate Facility

Attivaram, Andhra Pradesh

  • Greenfield facility for intermediates, key starting materials, and specialty chemicals
  • 75+ KL reactor capacity with three hydrogenators
  • High-vacuum distillation and cGMP clean-room capability
  • ISO and GMP certified operations

1,000 MT+/year capacity

API Facility

Medchal, Hyderabad

  • 40+ years of legacy in pharmaceutical manufacturing
  • Leading Ethambutol HCl (ETB) manufacturer for third-party sales
  • cGMP API facility with 50+ KL reactor capacity and clean room
  • State GMP certified operations

ETB 200 MT/year capacity

Chiral Separation

Advanced chiral resolution techniques for high-purity enantiomers

Hydrogenation

Up to 55 Kg operating pressure; heat-sensitive & exothermic reactions

High Vacuum Distillation

Fractionation column to separate close-boiling impurities

Nitro Compound Handling

Specialized in handling of Nitroparaffins and its derivatives (Nitromethane, Nitroethane etc.)

cGMP Clean Room

Dedicated clean rooms at both Attivaram and Medchal facilities

Scale-Up & Optimisation

Process development to achieve cost leadership at commercial scale

CDMO / CMO Services

Custom synthesis, route scouting and contract manufacturing

Safety & Compliance

State GMP (API) + ISO & GMP (intermediates) certifications

Explore Facilities

Reaction Capabilities

Discover our specialized chemistry at scale →

Photo Gallery

Take a visual tour of our sites →

Certificates

Review our quality and compliance credentials →